zł39.58
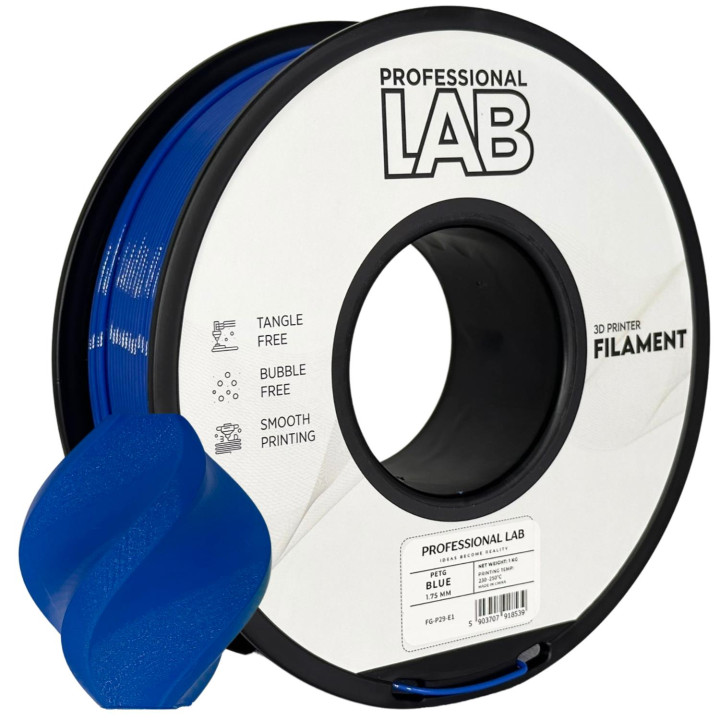
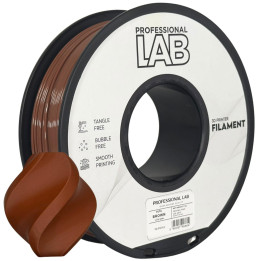
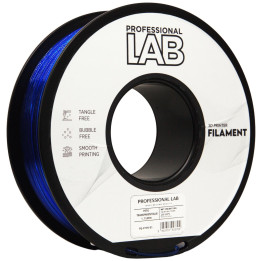
Filament PETG Prof. Lab 1.75mm 1kg Blue High-Strength images
Take your prints into the area of advanced mechanical and environmental applications. Professional filament Prof. Lab PETG in an intense, expressive Blue color is an advanced premium engineering material that perfectly combines the best features of the two most popular polymers. It offers structural strength and thermal resistance similar to ABS materials, while maintaining excellent dimensional stability and ease of printing known from traditional PLA.
The material is characterized by slight elasticity, which translates intoexceptional impact strength and resistance to cracking under the influence of dynamic stress. PETG is naturally 100% insensitive to moisture, water and a wide range of chemicals and acids. Thanks to minimal processing shrinkage, this filament adheres perfectly to the substrate and does not require the use of a closed working chamber. A saturated blue shade with a delicate, glass shine gives the models a professional look. It is an ideal choice for the production of functional parts, moving mechanisms, housings operating in difficult conditions, handles and all outdoor applications. The product works with most open FDM/FFF 3D printers.
Filament diameter: 1.75 mm (geometric tolerance: ± 0.03 mm) Color / Finish: Blue (Blue / With a slight shine) Plastic type: PETG (Polyethylene terephthalate with glycol) Net weight of the material: 1.0 kg (gross weight with packaging: ~1.3 kg) Nozzle Temperature (Nozzle): 220°C – 240°C Table temperature (Bed): 80°C – 90°C (heated bed absolutely required) Spool dimensions: Outer diameter: 195 mm | Centering hole: 75 mm Producer / Country of origin: Imagine s.c., Cholerzyn (Poland)
PETG is a material with very strong adhesion to some surfaces, which requires appropriate preparation of the working platform.
• Table surface protection: Due to the extremely strong adhesion of PETG to clean glass or smooth PEI boards, it is recommended to use separating agents (e.g. PVA glue, dedicated adhesive varnishes). This prevents damage to the table surface when removing the finished model.
• Cooling control: To obtain maximum mechanical strength and cohesion of the layers, it is recommended to limit the cooling airflow (suggested values: 20-50% depending on the geometry). Too intense airflow may weaken polymer bonds.
• Compatibility: Fully compatible with Prusa, Bambu Lab, Creality (Ender), Anycubic devices and other 3D printers supporting nozzle temperatures up to 240°C.
The filament is wound on a stable, stiff spool in a completely orderly manner, which prevents the line from crossing and tangling during many hours of work sessions. Each spool is factory-packed and hermetically packed in a thick barrier foil in a vacuum cover with an active moisture absorber (silica gel).
Tip: PETG plastics have a natural tendency to absorb moisture from the air superficially (hygroscopicity). After opening the package, it is recommended to store the spool in a dry place, a dedicated dry box container or a tight string bag with an absorbent. If the material becomes damp, it is worth drying it before printing (approx. 60°C for 4-6 hours), which will completely eliminate threading (stringing) and the formation of air bubbles in the structure of the walls.

Comments (0)
Your review appreciation cannot be sent
Report comment
Report sent
Your report cannot be sent